Chemical Process Reactor: Working Principle, Types & Selection
A chemical process reactor provides a controlled environment in which reactants are converted into products under defined process conditions. Reactor performance depends on factors such as reaction kinetics, residence time, mixing, heat transfer, temperature, pressure and fluid properties.
Depending on the process duty, reactor operation may be batch, semi-batch or continuous. Selecting the appropriate reactor concept requires understanding how the reaction behaves, how heat and mass must be transferred, and how those process requirements translate into practical equipment.
What Is a Chemical Process Reactor?
A chemical process reactor is equipment in which reactants are brought together under controlled process conditions so that a desired chemical transformation can take place. Depending on the process, important variables may include temperature, pressure, residence time, mixing, heat transfer, fluid properties and the contact between different phases.
Reactor operation may be batch, semi-batch or continuous. The reactor concept describes how materials enter, mix, react and leave the system, while the actual equipment configuration translates those process requirements into vessel geometry, heat-transfer surfaces, agitation, nozzles, instrumentation and controls.
The appropriate reactor arrangement therefore depends on the reaction kinetics, thermal duty, mixing requirement, phase behaviour, operating conditions and required production mode rather than on one universal vessel design.
How Does a Chemical Process Reactor Work?
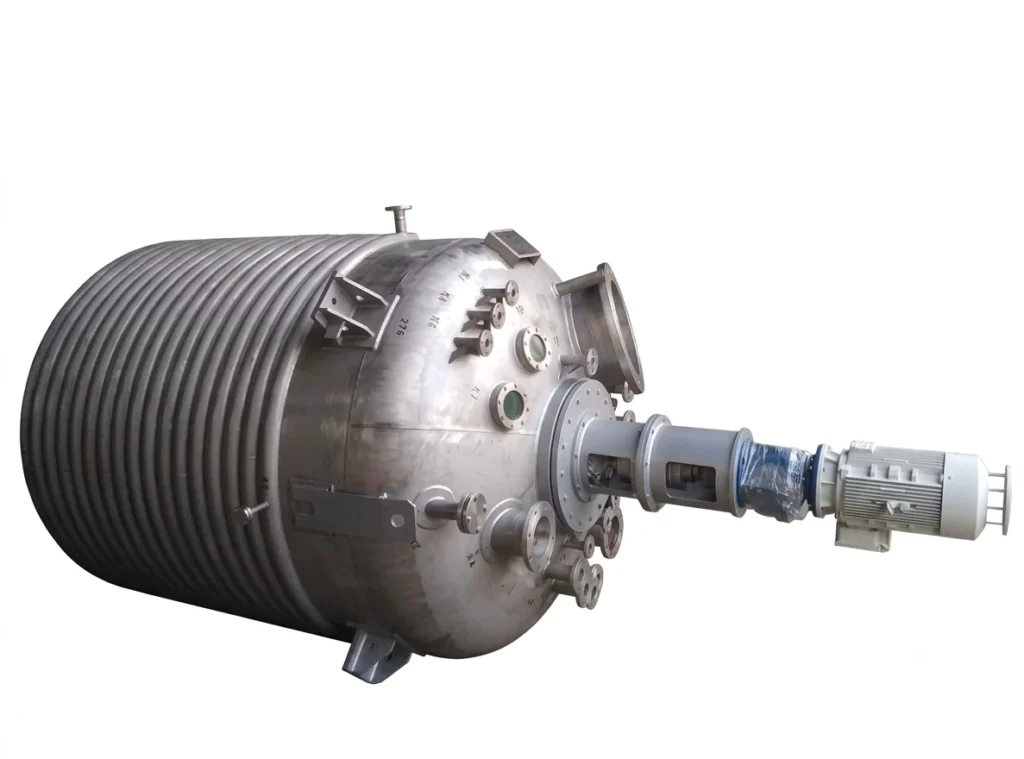
A chemical process reactor works by bringing reactants together under controlled conditions and maintaining the environment required for the desired reaction. Depending on the process, this may involve controlled feeding, mixing, heating or cooling, pressure management and sufficient reaction or residence time before the product is discharged.
Feed or Charge the Reactants
Raw materials are introduced according to the required process sequence. In batch operation, materials may be charged before the reaction begins, while semi-batch operation can use controlled or staged addition during the reaction.
Establish the Required Process Conditions
The reactor is brought to the required operating conditions. Heating or cooling may be applied through a suitable heat-transfer system, while pressure or vacuum is controlled where the process requires it.
Mix and Contact the Phases
Agitation can promote bulk circulation, temperature uniformity and contact between liquids, solids or gases. The required mixing intensity depends on fluid properties, phase behaviour and the objective of the process.
Control the Reaction
Temperature, pressure, feed rate, agitation and other relevant process variables are monitored and adjusted to keep the reaction within its defined operating conditions.
Provide the Required Reaction or Residence Time
The reacting material remains in the system for the time required by the process. In continuous reactors, residence-time behaviour depends on the reactor concept and flow pattern rather than on a simple batch hold period.
Discharge and Prepare for the Next Operation
Once the required process endpoint is reached, the product is discharged or transferred to the next process stage. Cleaning, inspection or preparation for the next batch depends on the product and operating procedure.
Batch, Semi-Batch and Continuous Reactor Operation
Chemical reactors can be operated in different ways depending on how reactants are introduced, how long material remains in the reaction system and how product is withdrawn. The operating mode affects process control, production scheduling, residence-time behaviour and the way heat and mass transfer requirements are managed.
Batch Operation
In a batch reactor, a defined quantity of reactants is charged, processed for a specified period or until the required endpoint is reached, and then discharged. Batch operation is useful where recipes change, production is campaign-based, or the process requires clearly separated reaction stages.
Semi-Batch Operation
In semi-batch operation, one or more materials are added or removed while the reaction is in progress. Controlled addition can be useful when feed rate influences reaction rate, heat release, selectivity, gas evolution or other process behaviour.
Continuous Operation
In continuous operation, reactants are fed and products are withdrawn while the reactor remains in service. Reactor performance depends on the flow pattern, residence-time distribution, reaction kinetics and the degree of mixing within the system.
Operating mode and reactor type are related but not identical. For example, CSTR and PFR describe different continuous-reactor concepts and flow behaviour; they are explained separately in the next section.
Types of Chemical Process Reactors
Batch and semi-batch operation are described in the previous section. Within continuous processing, two important ideal reactor concepts are the Continuous Stirred-Tank Reactor (CSTR) and the Plug Flow Reactor (PFR). They differ primarily in how mixing, flow and composition are represented within the reaction system.
Continuous Stirred-Tank Reactor (CSTR)
A Continuous Stirred-Tank Reactor (CSTR) is a continuous-reactor concept in which reactants enter and product leaves while the reactor contents are assumed, in the ideal model, to be completely mixed.
Under this ideal assumption, concentration and other bulk properties are uniform throughout the reactor, and the outlet composition corresponds to the composition within the reactor. Actual performance depends on mixing, reaction kinetics, residence-time behaviour and process conditions.
Plug Flow Reactor (PFR)
A Plug Flow Reactor (PFR) is a continuous-reactor concept in which material moves through the reaction zone with limited axial back-mixing in the ideal model.
Because material progresses along the flow path, composition and temperature may change with position through the reactor. Reactor performance therefore depends on reaction kinetics, residence time, heat transfer, flow behaviour and fluid properties.
Batch vs CSTR vs PFR — Key Differences
Batch reactors, Continuous Stirred-Tank Reactors (CSTRs) and Plug Flow Reactors (PFRs) represent different ways of carrying out and modelling a chemical reaction. Their main differences relate to material flow, mixing assumptions, residence-time behaviour and how composition changes during the reaction. The appropriate concept depends on the reaction kinetics and overall process requirement.
| Factor | Batch Reactor | CSTR | PFR |
|---|---|---|---|
| Operation | Processes a defined charge over time. | Continuous feed and continuous product withdrawal. | Continuous feed and continuous product withdrawal. |
| Ideal Mixing / Flow Model | Often treated as well mixed within the batch. | Ideally completely mixed. | Ideally limited axial back-mixing. |
| Composition Behaviour | Changes with reaction time. | Ideally uniform throughout the reactor at a given steady state. | Changes progressively along the direction of flow. |
| Residence-Time Concept | Material remains in the reactor for the batch reaction period. | Material has a distribution of residence times around a mean residence time in a real continuous stirred system. | Material progresses through the reactor along the flow path. |
| Process Control | Process variables are followed through the batch cycle. | Conditions are controlled during continuous operation. | Process conditions may vary with position along the reactor. |
| Production Pattern | Discrete batches. | Continuous production. | Continuous production. |
| Process Suitability | Useful where recipe flexibility, staged operations or separated batches are required. | Considered where continuous operation with strong internal mixing is appropriate. | Considered where progressive reaction along the flow path is appropriate. |
| Key Design Consideration | Batch sequence, reaction time, mixing and thermal duty. | Mixing quality, residence-time behaviour, kinetics and heat transfer. | Flow distribution, kinetics, residence time and heat transfer along the reactor. |
How Is a Chemical Process Reactor Selected?
Selecting a chemical process reactor starts with the process requirement, not with a predefined vessel type. The reactor concept and equipment configuration should be based on reaction behaviour, production mode, fluid properties, thermal duty and the operating conditions that must be controlled.
Reaction Kinetics & Process Objective
Reaction rate, conversion target, selectivity, reaction pathway and whether the process is exothermic or endothermic influence the reactor concept and required reaction or residence time.
Operating Mode & Feed Strategy
The process may require batch, semi-batch or continuous operation. Feed sequence, staged additions, product withdrawal and production scheduling help determine how the reactor should operate.
Fluid Properties & Phase Behaviour
Viscosity, density, solids content, gas involvement, miscibility and changes in rheology during the reaction affect mixing, mass transfer and the internal flow behaviour required from the reactor system.
Heat-Transfer Requirement
Heating, cooling and reaction heat release or absorption must be evaluated together with utility conditions, available heat-transfer area, fouling tendency and the effect of mixing on thermal performance.
Pressure, Temperature & Material Compatibility
Operating and design pressure, vacuum conditions, temperature range and chemical compatibility influence vessel construction, sealing, materials of construction and the mechanical design basis.
Control, Cleaning & Scale-Up Requirements
Instrumentation, automation, sampling, cleaning method, batch repeatability and scale-up requirements should be defined before the final equipment configuration is selected.
Mixing and Mass Transfer in Chemical Reactors
Mixing influences how reactants, heat and dispersed phases are distributed inside a chemical reactor. Its purpose is not simply to keep material moving; the required mixing pattern depends on the reaction system, fluid properties and whether the process involves liquid blending, solids suspension, gas dispersion or heat-transfer duty.
Concentration Uniformity
Adequate circulation helps reduce concentration differences within the reactor so that reactants are distributed more consistently through the process volume.
Heat-Transfer Support
Mixing affects the process-side fluid film near the vessel wall or heat-transfer surface. Better circulation can improve temperature uniformity and support heating or cooling performance, but the actual result depends on fluid properties, geometry and operating conditions.
Solid–Liquid Contact
Where solids are present, mixing may be required to keep particles suspended, improve contact with the liquid phase or limit settling. The required agitation depends on particle properties, solids loading and fluid behaviour.
Gas–Liquid Contact
For gas–liquid reactions, mixing can influence gas dispersion, bubble distribution and the available interfacial area for mass transfer. The required system depends on gas rate, reaction duty and vessel configuration.
Viscosity & Rheology
As viscosity increases or rheology changes during a reaction, circulation and mixing behaviour can change significantly. Agitation therefore needs to be considered together with the expected fluid-property range across the process.
Mixing requirements are process-specific. Impeller family, speed, diameter, number of stages and drive power should not be selected from viscosity alone. Vessel geometry, phase behaviour, heat-transfer duty, solids or gas loading and shear sensitivity also matter.
For detailed impeller, shaft, drive, seal and stage configuration, see our Industrial Agitator page.
Heat Transfer and Temperature Control in Chemical Reactors
Temperature control can directly affect reaction rate, selectivity, product quality and process safety. A reactor may need to add heat, remove heat, maintain a controlled temperature, or perform different thermal duties at different stages of the process.
Heating and Cooling Duty
The required thermal system depends on how much heat must be added or removed, how quickly the process temperature must change, and whether the reaction itself releases or absorbs heat.
Heat-Transfer Area
Available heat-transfer surface influences how thermal energy is exchanged between the process and utility side. The required area depends on the thermal duty, temperature driving force, fluid properties, fouling and operating conditions.
Utility Conditions
Steam, hot water, thermal fluid, cooling water, chilled water or other utilities may be used depending on the process. Utility temperature, pressure, flow rate and availability form part of the thermal design basis.
Mixing and Temperature Uniformity
Agitation can influence circulation near heat-transfer surfaces and help reduce temperature gradients within the reactor. The actual effect depends on vessel geometry, fluid behaviour, agitation and the thermal arrangement.
Exothermic and Endothermic Reactions
For an exothermic reaction, the system must be able to remove reaction heat at the required rate. Endothermic processes may require controlled heat input. Feed strategy and control philosophy may also form part of the thermal-management approach.
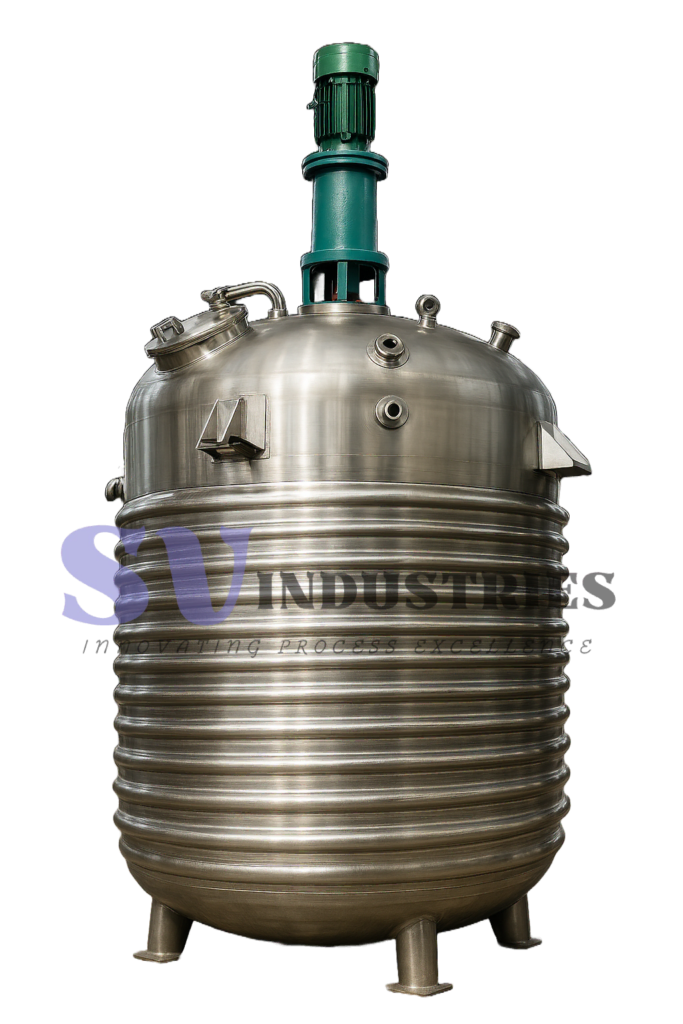
Thermal performance is process-specific. Jacket, limpet or other heat-transfer arrangements should not be selected from a single U-value or general rule of thumb. Final selection depends on heat duty, utility conditions, allowable pressure and temperature, fouling, vessel geometry, mixing and the required operating cycle.
For equipment-specific thermal configurations, see SS Jacketed Vessel and Limpet Coil Reactor Vessel.
Process Variables That Define Reactor Duty
A chemical reactor cannot be defined by capacity alone. Its process duty is established by the conditions the equipment must maintain throughout the reaction, including temperature, pressure, residence time, fluid behaviour, phase interaction and heat load. These variables form the process basis from which the reactor configuration is developed.
Reaction Temperature
The required operating temperature and allowable temperature variation influence reaction behaviour, thermal duty, utility selection and the equipment required to maintain controlled conditions.
Pressure or Vacuum
Operating pressure, vacuum conditions and possible pressure changes during the process affect the mechanical design basis, sealing arrangement, instrumentation and safety provisions.
Reaction or Residence Time
The required time for reaction or material residence affects production capacity, batch scheduling and, for continuous systems, the relationship between reactor volume and flow rate.
Fluid Properties
Density, viscosity, rheology, solids content and changes in these properties during the reaction influence circulation, mixing, heat transfer and equipment configuration.
Phase Behaviour
A reaction may involve liquid–liquid, solid–liquid, gas–liquid or other multiphase contact. The phases present and the required contact between them influence mixing and mass-transfer requirements.
Heat Load
The amount and rate of heat generated, absorbed, added or removed form part of the reactor’s thermal duty. Both reaction heat and sensible heating or cooling requirements should be considered.
Feed and Discharge Conditions
Feed rate, feed temperature, staged additions, solids introduction, gas addition and product withdrawal can affect reaction control and the required arrangement of nozzles, internals and controls.
Process Control Requirements
Temperature, pressure, level, flow, agitation, pH or other variables may need to be monitored or controlled depending on the process. The required control philosophy should be defined as part of the process basis.
Reactor duty is project-specific. Two reactors with the same nominal capacity can require very different agitation, heat-transfer surfaces, pressure design, controls and materials because their process conditions are different.
From Reactor Concept to Fabricated Equipment
A process reactor model defines how the reaction is intended to behave, but the physical equipment must translate that process basis into a practical vessel system. The final configuration may combine vessel geometry, heat-transfer surfaces, agitation, nozzles, instrumentation, controls and materials of construction according to the required duty.
Vessel Configuration
Working volume, vapour space, orientation, vessel proportions, head arrangement and internal clearances are determined from the process and mechanical design requirements rather than from capacity alone.
Heat-Transfer Arrangement
Where heating or cooling is required, the vessel may incorporate a jacket, limpet/half-pipe coil or another suitable thermal arrangement. Selection depends on the thermal duty, utilities, operating conditions and mechanical design basis.
Agitation System
Where mixing is required, the agitator configuration is developed from the process objective, fluid properties and vessel geometry. Impeller type, shaft arrangement, stages and drive requirements are therefore duty-specific.
Nozzles & Process Connections
Feed, discharge, vent, instrumentation, sampling and utility connections must be arranged around the operating sequence, accessibility and process requirements.
Instrumentation & Controls
Temperature, pressure, level, flow, agitation or other process variables may require measurement, control, interlocks or automation depending on the operating philosophy.
Materials & Mechanical Design
Material selection, vessel thickness, supports, sealing and fabrication details depend on chemical compatibility, temperature, pressure or vacuum conditions and the applicable mechanical design basis.
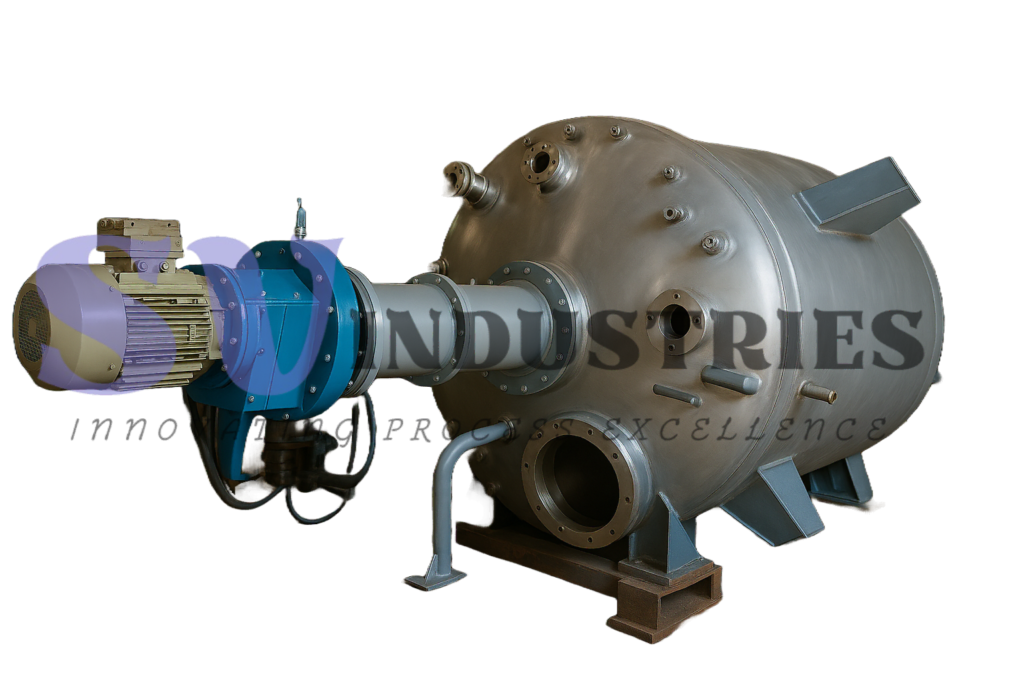
The process reactor concept and the fabricated reactor vessel are related, but they are not the same thing. A CSTR or batch-process requirement does not by itself define the vessel construction, thermal system, agitation or mechanical design.
For equipment-specific details, see our Industrial Chemical Reactor, Reactor Vessel and Industrial Agitator pages.
Information Required Before Selecting Reactor Equipment
Once the reactor concept is understood, the next step is to define the process data required to configure the actual equipment. Capacity alone is not enough; the supplier or design engineer needs information about the material being processed, operating conditions, thermal duty, mixing requirement and production sequence before the vessel configuration can be finalized.
Capacity & Operating Volume
Provide the required working volume, expected filling level and, where known, total vessel volume or required free space above the process liquid.
Process Mode & Batch Sequence
Define whether the process is batch, semi-batch or continuous, together with the charging sequence, staged additions, hold periods and discharge requirements.
Process Media & Composition
Identify the liquids, solids, gases or solvents involved, along with concentration ranges and any significant changes in composition during the reaction.
Temperature & Pressure Conditions
Provide normal operating temperature and pressure, required design limits, vacuum conditions if applicable, and any important temperature or pressure changes during the operating cycle.
Heating & Cooling Requirement
Define the required heat-up, reaction hold and cool-down duties where available, together with utility temperatures, pressures and available heating or cooling media.
Fluid Properties & Phase Behaviour
Viscosity, density, solids loading, particle characteristics, gas rate, miscibility and expected rheology changes help establish the mixing and mass-transfer requirements.
Mixing Objective
State what the agitation system must achieve—for example blending, solids suspension, gas dispersion, temperature uniformity or controlled circulation—rather than selecting an impeller from RPM alone.
Materials, Cleaning & Product Contact
Chemical compatibility, corrosion concerns, required product-contact material, cleaning method, surface-finish requirement and any hygienic or validation needs should be identified.
Instrumentation & Automation
Specify the process variables that must be measured or controlled and the required level of automation, interlocking, data logging or operator control where applicable.
Site & Integration Requirements
Where relevant, provide available utilities, space or access limitations, installation constraints and interfaces with upstream or downstream process equipment.
Chemical Process Reactor Applications
Chemical process reactors are used across industries where materials must be reacted, mixed, heated, cooled or contacted under controlled process conditions. The reactor configuration varies with the chemistry, operating mode, phase behaviour, thermal duty and production requirements of each application.
Chemical & Specialty Chemical Processing
Reactor duties may include esterification, neutralization, condensation, sulfonation and other batch or continuous chemical transformations requiring controlled process conditions.
Pharmaceutical & Fine Chemical Processing
Reactors may be used for synthesis, crystallization, controlled additions and other process steps where temperature, mixing, cleanliness and repeatability are important.
Dyes & Intermediates
Applications can include coupling, diazotization, neutralization and related reactions involving controlled addition, mixing and temperature management.
Resins, Polymers & Adhesives
Polymerization, condensation and resin-processing duties can involve changing viscosity, heat release and significant changes in mixing behaviour during the reaction.
Agrochemical & Formulation Processes
Reactor duties may include reaction, neutralization, formulation and suspension-based processes involving solids, liquids or staged additions.
Paints, Coatings & Pigment Systems
Process equipment may be used for blending, let-down, reaction or dispersion-related duties depending on the required chemistry and product characteristics.
Surfactants & Home-Care Chemicals
Applications may involve saponification, neutralization, controlled heating or cooling, blending and other liquid-processing operations.
Petrochemical, Oleochemical & Related Processes
Reactor systems may be used for suitable synthesis, transesterification, phase-contacting or other process duties where temperature, residence time and fluid behaviour must be controlled.
Frequently Asked Questions About Chemical Process Reactors
What is a chemical process reactor?
A chemical process reactor is equipment in which reactants are brought together under controlled conditions so that a desired chemical transformation can occur. Important process variables may include temperature, pressure, residence time, mixing, heat transfer and phase contact.
How does a chemical process reactor work?
A reactor provides the conditions required for a reaction by controlling how materials are introduced, mixed, heated or cooled, retained and discharged. The exact sequence depends on whether the process is batch, semi-batch or continuous.
What is the difference between batch and continuous reactors?
A batch reactor processes a defined quantity of material through a reaction cycle before discharge. In continuous operation, reactants are supplied and products are withdrawn while the reactor remains in service.
What is a Continuous Stirred-Tank Reactor (CSTR)?
A CSTR is an ideal continuous-reactor model in which the contents are assumed to be completely mixed. Under the ideal assumption, the outlet composition corresponds to the composition within the reactor.
What is a Plug Flow Reactor (PFR)?
A PFR is an ideal continuous-reactor model in which material moves through the reaction zone with limited axial back-mixing. Composition and temperature may change progressively along the direction of flow.
How is a chemical reactor type selected?
Reactor selection depends on the reaction kinetics, operating mode, residence-time requirement, phase behaviour, mixing need, thermal duty, pressure and temperature conditions, and overall production objective.
Why is mixing important in a chemical reactor?
Mixing can influence concentration uniformity, heat transfer, solids suspension, gas dispersion and mass transfer. The required mixing system depends on the fluid properties, vessel geometry and actual process duty.
Why is temperature control important in reactor operation?
Temperature can affect reaction rate, selectivity, product quality and process safety. A reactor may therefore require controlled heating, heat removal or temperature holding during different stages of the process.
Related Reactor and Mixing Equipment
A chemical process reactor is part of a wider equipment system. Depending on the project, the process requirement may lead to a dedicated reactor vessel, thermal configuration or agitation system. The following pages provide more detailed information on the equipment side of reactor design and fabrication.
01
Industrial Chemical Reactor
For manufacturing capability, materials, fabrication, testing and project-specific industrial reactor enquiries.
02
Reactor Vessel
Custom reactor vessel design and fabrication for project-specific mechanical and process requirements.
03
Industrial Agitator
Agitator systems configured for blending, suspension, heat transfer and other process mixing duties.
04
SS Jacketed Vessel
For projects where a conventional annular jacket may be considered instead of an external half-pipe or limpet arrangement.
Discuss Your Reactor Requirement
If you are evaluating a reactor for a new process, replacement unit or capacity expansion, the next step is to define the actual process basis. Share the available information on capacity, process media, operating mode, temperature, pressure or vacuum, thermal duty, mixing requirement, materials and automation needs so the equipment configuration can be reviewed against the intended duty.